• Tel +44(0)1274 617021

High-Integrity Heat
Exchangers & Pressure
Equipment. Built for
Reliability.

Safe Professional Innovative

For over 50 years, we’ve combined advanced thermal design with precision British manufacturing. Whether you require standard process efficiency or equipment engineered for complex, high-specification environments, we deliver thermal solutions built to last.

Engineering Excellence for Every Process Line

Graham Hart Process Technology Ltd is a world leader in the design and manufacture of bespoke heat transfer and specialist pressure equipment. With more than five decades of experience, we engineer every unit to precise client requirements, ensuring optimal performance, safety and longevity in mission-critical environments.

Our team of process and mechanical engineers provide deep technical understanding, supported by advanced software, rigorous risk assessment and fully integrated digital management systems. Whether your operation requires reliable, hygienic systems for high-volume production or custom designs capable of handling extreme pressures and corrosive media, our equipment is built to deliver long-term reliability and confidence.

Since 2016, we have maintained a 100% On Time In Full delivery record, demonstrating our commitment to quality, professionalism and customer success.

Single Suppy Chain
Design, procurement, manufacture, testing and certification all in-house.
Precision Engineering
From advanced process modelling to large-scale machining up to 2.3 m diameter and 460 mm thick.
Proven Reliability

Over a decade supplying subsea heat transfer innovations.

Global Trust

Preferred partner to leading organisations including Airbus, BOC, GE, and Tata.

Heat Exchanger Solutions

Shell & Tube Heat Exchangers

Shell & Tube Heat Exchangers

Robust and versatile units engineered for high-pressure, high-temperature and corrosive environments.

Air Cooled Heat Exchangers

Air Cooled Heat Exchangers

Efficient cooling systems ideal for water-scarce locations and remote operations.

Crossflow & Heat Recovery Systems

Crossflow & Heat Recovery Systems

Custom designs for stack gas recovery, combustion air preheating and process fluid heating.

Bespoke Engineered Equipment

Bespoke Engineered Equipment

Fully customised heat transfer solutions designed around your process, duty and operational environment
Graham Hart Double Pipe Heat Exchanger

Double Pipe Heat Exchangers

Optimised for space-constrained and high-duty applications, and provide a practical and efficient alternative to traditional shell and tube designs.
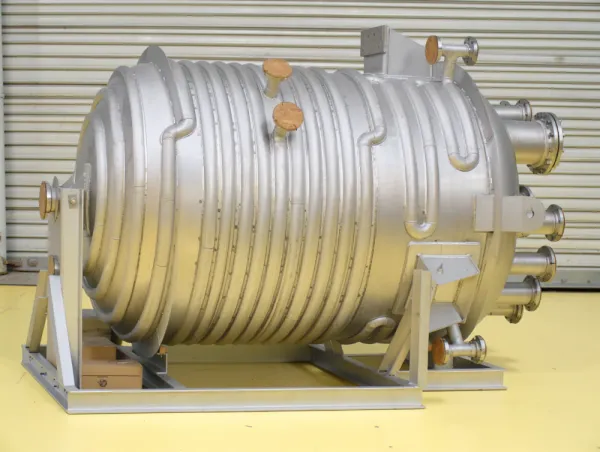
Graham Hart Reactor Vessel

Reactor Vessels

Provde precise thermal control for critical processes, supporting high-pressure reactions in controlled operating conditions.

Sectors We Support

From high-efficiency food and drink processing lines to high-specification nuclear and subsea applications, we design and manufacture heat transfer solutions tailored perfectly to your industry's standards.

Industry Sectors:

Nuclear

Nuclear

Safety-driven designs meeting the highest integrity standards.

Oild & Gas

Oil & Gas

Proven performance from FPSO vessels to 3 km subsea operations.

Chemical

Chemical

Robust heat transfer and pressure solutions for demanding, corrosive chemical processes.

Petrochemical

Petrochemical

Precision-engineered for corrosive and high-temperature processes.

Food & Drink

Food & Drink

Reliable, hygienic systems tailored to demanding production facilities.

Pharmaceutical

Pharmaceutical

Critical equipment supporting sterile and controlled environments.

Insights from Our Engineers

Expert guidance, case studies and technical updates.
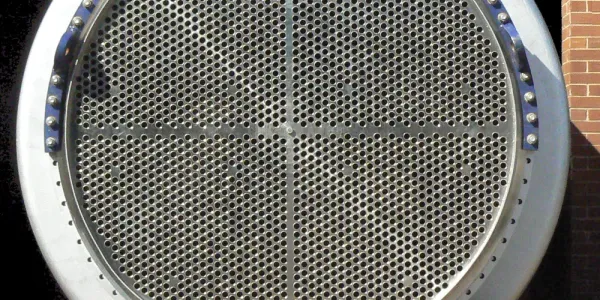
Close up of the end of a Heat Exchanger

Boosting Cooling Performance for an Agriculture Client

The client had an under performing conventional cooler, restricted by space constraints, operating under vacuum conditions. They needed better performance, both with higher flow rate and lower temper…
Published: 16 May 2026
Category: Case Studies
Heat Exchanger technical drawings

Efficient Condensate Cooling

A food and beverage client required three air cooled heat exchanger units to provide reliable condensate cooling in a challenging site environment.
Published: 16 May 2026
Category: Case Studies
Shell and Tube Heat exchanger for a chemical manufacturer

Increasing Process Throughput

A chemical manufacturing client was looking to replace a unit that had been in service for over 20 years.
Published: 16 May 2026
Category: Case Studies
Shell and Tube Heat Exchanger Efficiencies

Unlocking Process Efficiency in Heat Exchangers

Graham Hart will host a special breakfast event exploring how thermal engineering choices directly impact plant efficiency, sustainability goals, and bottom-line performance.
Published: 02 September 2026
Category: News
Cyber Essentials Certified Plus Accreditation logo

Graham Hart Achieves Cyber Essentials Plus Accreditation

We're pleased to share that Graham Hart Process Technology has been awarded Cyber Essentials Plus certification, the UK government-backed standard that recognises organisations with strong, independe…
Published: 10 June 2026
Category: News
Photo of Chris Hart names among UK's Top Manufacturing Leaders

Graham Hart Process Technology MD Named Among the UK’s Top Manufacturing Leaders

We’re proud to share some fantastic news. Our Managing Director, Chris Hart, has been named one of the UK’s most inspiring manufacturing leaders in the Manufacturing 100 Awards 2025, organised annual…
Published: 13 December 2025
Category: News

Ready to Discuss Your Project?

Our engineers are here to help you develop safe, reliable and efficient heat transfer solutions tailored to your process.

Trusted by Industry Leaders

Our solutions support world-class operations across aerospace, pharmaceuticals, energy, food and national infrastructure programmes.

UKAS AND ISO 45001UKAS AND ISO 14001UKAS AND ISO 9001gbc accredited stampASME U Stamp HolderNational Board RegisteredCyber Essentials Certificate PlusF4N - Fit For NuclearF4H2 - Fit for HydrogenF4CCUS - Carbon Capture Usage & Storage

It was so quiet, I hadn’t realised your Air Cooled Heat Exchanger was operating.
Major Industrial Client
We didn’t believe anyone could design a unit to do this duty—now the rest of the plant can’t keep up with your equipment.
Operations Manager
Your 50-tonne unit fit like a glove… the riggers finished in a day instead of a week.
Project Engineer